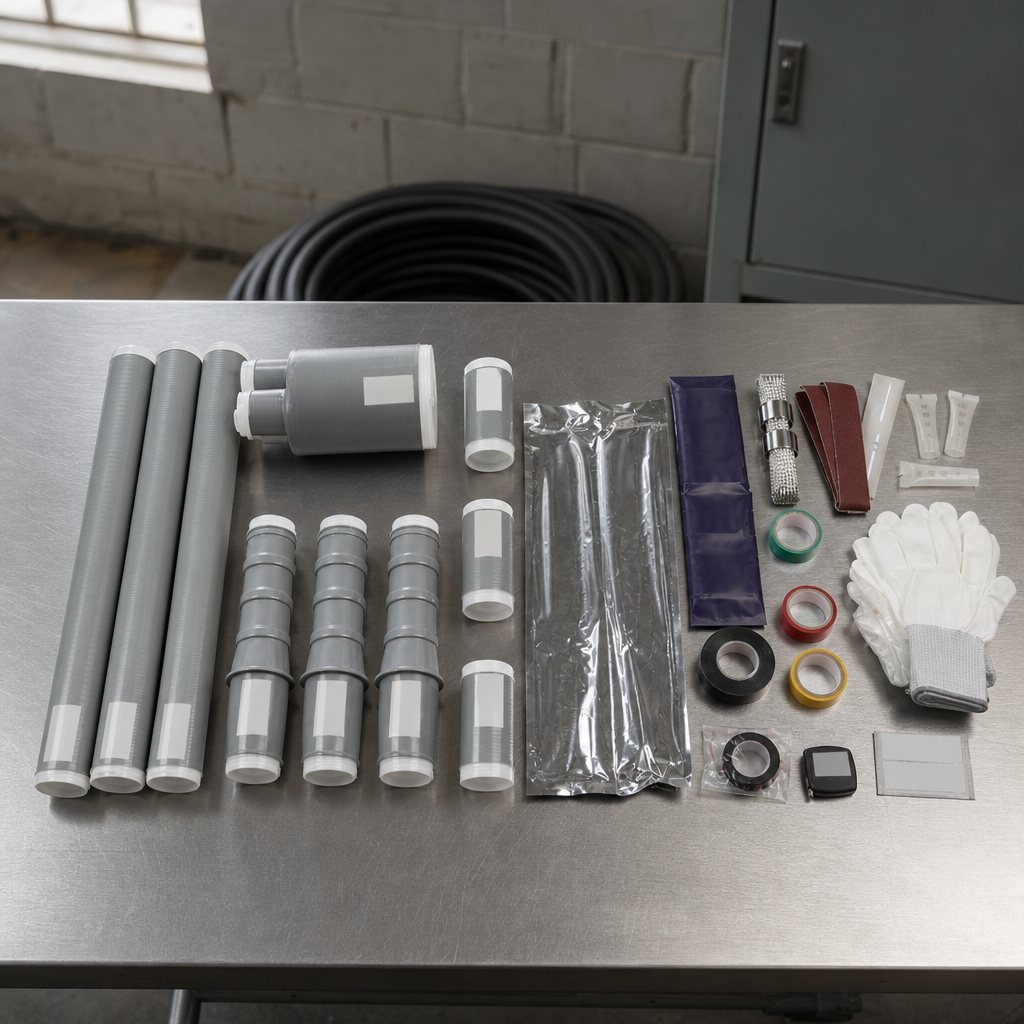
A cable joint kit is the packaged set of parts used to join two lengths of power cable permanently: the joint body with its stress-control and insulation components, the screen and armour bonding materials, and the small consumables that make the joint up. The kit is matched to one cable — a voltage class, a conductor cross-section range, a core count and an insulation diameter — so everything in the box belongs to that single joint. Mains-power distribution networks use them wherever a cable run is longer than a drum, or wherever a faulted section has to be cut out and replaced.
Getting the kit right is mostly a specification exercise, and it is one that goes wrong in predictable ways. Joints are the weakest point in an otherwise sound cable run, which is why utilities write detailed material specifications for them and why a joint that is merely "the right size" can still fail in service. This guide covers what a joint kit contains, how a joint differs from a termination, which joint technology suits which environment, and the clauses a buyer should pin down in an RFQ.
What Is a Cable Joint Kit?
A joint is a cable accessory that connects two cables to each other. It has to restore everything the cable did before it was cut: the conductor path, the insulation, the electric-field distribution at the point where the insulation screen is cut back, the metallic screen, and — on armoured cable — the armour. A joint kit supplies the materials to do all of that in one matched package.
A kit differs from a termination in where it sits, not in how carefully it must be chosen. A termination is at the end of a cable, where the cable meets a transformer, a switchgear panel, a metering cubicle or an overhead line. A joint is mid-span, buried in a trench or laid in a duct, between two lengths of the same cable. Both are sold as kits. Both are sized to the cable. Neither can be selected from the voltage alone.
That last point decides most purchase orders. Cable cross-section, conductor material, core count, insulation type and the diameter over the insulation all change which kit fits, so an RFQ that says only "11 kV joint" cannot be quoted accurately. The published ordering tables for these products are indexed by cable cross-sectional area for exactly that reason.
Cable Joint vs Cable Termination: What Is the Difference?
The two are often bought on the same requisition and confused in the same sentence. The distinction is worth stating plainly, because it determines whether a cable run can be tested, sectionalised and repaired the way the network designer intended.
| Cable joint | Cable termination | |
|---|---|---|
| Where it sits | Mid-span, between two lengths of cable | At the cable end, where the cable meets equipment or an overhead line |
| What it connects | Cable to cable | Cable to apparatus or to an air-insulated conductor |
| Typical location | Joint bay, trench, duct, manhole, cable room floor | Transformer or switchgear cable box, metering cubicle, pole-top |
| Main construction concern | Rebuilding the screen, the stress control and the moisture barrier over the joint body | Controlling the field at the point where the screen is cut back, and sealing against the environment |
| Consequence if it is wrongly sized | Cannot be assembled over the cable, or will not close down onto the insulation | Will not enter the cable box, or the creepage distance to earth is inadequate |
A utility specification states the same distinction in its definitions: a straight joint "makes a connection between two cables", a branch joint connects a branch cable to a main cable, and a transition joint connects cables whose insulation type, conductor material or cross-section differ. Those three definitions cover almost every mid-span accessory a distribution project will order.
What Is Inside a Joint Kit?
Kits differ between technologies, but the bill of materials follows the same logic — one item for each function the cable performed before it was cut:
- Conductor connection. A compression or mechanical connector for each core, sized to the conductor material and cross-section.
- Insulation and stress control. The joint body itself — pre-expanded elastomeric sleeves, heat-shrink tubes or a factory-moulded body — plus the field-grading parts that control the stress where the screen is cut back.
- Screen and armour continuity. Copper braid, mesh or tape to rebuild the metallic screen, and bonding materials to reconnect the armour. Screen continuity is not cosmetic: it is what carries fault current and keeps the joint's earth path intact.
- Sealing and moisture control. Sealing mastic, filler gum, wrap-around sleeves or heat-shrink outer jackets, depending on whether the joint is in air, in a duct or directly buried.
- Consumables and tooling. Cleaning wipes or solvent, abrasive strips, tape, gloves, and — in heat-shrink kits — the torch and heat-shield materials the method needs.
The consumables are a useful signal when comparing quotations. A kit that omits the cleaning materials, the abrasive or the bonding braid is not cheaper; it has moved part of the job onto the installer, and the installer's improvisation is what the accessory maker was trying to remove.
Which Joint Technology Should You Specify?
Three technologies cover almost all distribution work, and the trade-off between them is about the installation, not about the electrical result when all three are done correctly.
| Heat-shrink | Cold-shrink (pre-expanded) | Pre-moulded | |
|---|---|---|---|
| How the body is formed | Tube shrunk onto the cable with a torch | Elastomeric sleeve pre-expanded on a removable core; the core is unwound and the sleeve contracts onto the cable | Factory-moulded insulation body with controlled geometry |
| Heat source needed | Yes — open flame or heat gun | No | No |
| Dependence on installer technique | High: correct heating, even shrinkage and surface preparation all matter | Lower: constant radial pressure is built into the material, and there are fewer steps to get wrong | Low for the body, but the body must suit the cable diameter closely |
| Where it is usually chosen | Familiar, widely stocked, easy to re-order | Harsh or restricted environments, and anywhere a hot-work permit is a problem | Repeat work on a known cable type |
Vendor technical comparisons make the same argument in different words. A pressure-testable elastomeric (cold-shrink) system is described as shrinking firmly onto the cable and providing an active seal that does not lose pressure as the cable heats and cools, and as needing no special tools or heat source — while heat-shrink is characterised by more installation steps and more room for installation error, with uneven heat application named as a specific risk to wall thickness and life expectancy.
That does not make heat-shrink a poor choice. It makes it a choice that depends on the workmanship available. If the same crew will install two hundred joints on a rural feeder programme, the technology that removes the torch and the operator's judgement is the one that reduces variance in the finished network.
How Do You Choose the Right Joint Kit Size?
Manufacturers publish ordering tables that map each cable joint kit model to a cable cross-sectional area band, and those bands are the fastest way to specify the correct item. In an LV multicore range, for example, one model may be the correct kit for 10–16 mm² three-core cable, the next for 25–50 mm², and so on up through 500–630 mm², with the set weight rising slightly across the range. Nahu Group publishes its cold-shrink range the same way — each model listed against a voltage level and a cable cross-section band, so the row for the cable can be identified before the RFQ is issued. Higher-voltage single-core and three-core terminations are tabulated the same way, again against conductor cross-section.
Four data points decide which row you are on:
- Conductor cross-sectional area. This is the primary index. It is also where mixed conductor lists go wrong: the kit must suit the actual cross-section, not the nominal rating of the cable.
- Number of cores. Joint kits are built for the core count of the cable. Reusing a four-core kit on a five-core cable, or the reverse, is not a workaround.
- Insulation type and outer diameter over the insulation. Two 240 mm² cables of the same voltage class can differ in the diameter the sleeve must close onto.
- Conductor material. Aluminium and copper connectors are different products. So is the correct joint for an aluminium-to-copper transition.
Armoured cable adds one more question: whether the kit includes the armour bonding and continuity parts, and whether the joint is intended for direct burial where the water table is high. Whichever way the kit is chosen, the sizing decision should be recorded in the requisition — the next person to repair that joint needs to know exactly what is down there.
What Does a Joint Kit Need to Prove?
Cable accessories are not covered by the cable standard alone. In the IEC system, the cable itself and the accessory are addressed by different parts of the same family: the cable part specifies construction, dimensions and test requirements for extruded-insulation power cables up to 30 kV, while accessory test requirements and accessory test methods sit in their own documents. Buyers writing a specification should name the document for the accessory, separately from the document for the cable.
The test regime a joint is normally judged on is the same one a cable faces, applied to a made-up assembly: AC voltage withstand, partial discharge, lightning impulse, thermal cycling and short-circuit testing of the screen, plus a screen resistance measurement. The point of running them on an assembly is obvious — the joint is where the workmanship is, and a laboratory-made joint is the only way to isolate the accessory from the installation.
In practice, a buyer wants three things on the table before the order: the standard (and edition) the accessory is type-tested to, which class within that standard applies, and a type-test report that names the kit model rather than the family. A report that covers a different joint body or a different voltage class is not evidence about the kit you are buying. Where the network is designed to IEEE practice rather than IEC practice, the joint standard changes and the evidence has to change with it — the two systems are not interchangeable on paper, even where the hardware looks the same.
Where Do Cable Joints and Terminations Fail?
Accessory reliability is dominated by things that happen on site rather than in the factory. A specialist accessory supplier's failure-mode list names the usual suspects: improper accessory selection, instructions that are difficult to follow, workmanship, the number of installation steps, how the accessory is delivered to the cable, the tolerances and product design, environment, and the training and support behind the crew.
Two physical mechanisms sit behind most of that list. The first is the field concentration where the screen is cut back: unless the stress-control parts are fitted exactly as the instructions require, local stress at that point accelerates ageing or triggers failure. The second is moisture and voids. Cold-shrink silicone conforms well to cable bends precisely because it maintains pressure against the insulation over the life of the joint, which is what keeps voids and moisture ingress out.
Both point to the same purchasing conclusion. A kit that removes steps, arrives with everything the method needs and is supplied with installation training is a better risk than a cheaper kit that assumes a highly skilled jointer. On a distribution network, joint failure is not a warranty conversation — it is a digging job.
What Should a Joint Kit RFQ State?
An RFQ that lists these items can be quoted without a round of clarification, and it protects the buyer when the goods arrive:
- Voltage class (for example 0.6/1 kV or 26/35 kV), system earthing, and whether the joint is for a single-core or multicore cable
- Conductor material and cross-sectional area for every cable the joint may be used on, including any transition between different sizes or materials
- Insulation type and the diameter over the insulation or over the metallic screen
- Screen and armour construction, and whether armour continuity and bonding parts are required in the kit
- Installation environment: indoor cable room, outdoor joint bay, duct, or direct burial, and the burial conditions where relevant
- Joint technology and whether a heat source is permitted on site
- The standard and class the accessory is to be type-tested to, plus the type-test report for the model offered
- Contents list per kit, packing, and whether installation training or a jointing procedure is supplied
Add one sentence to the RFQ about the jointing crew: whether they are trained on the proposed system, and whether the supplier will support a first-installation inspection. Accessory makers publish installation-sensitive comparisons precisely because the answer changes the risk profile of the whole cable run.
Four Specification Mistakes That Appear on Every Project
- Specifying a joint by voltage only. Cross-section, core count, insulation diameter and conductor material decide whether the sleeve will even close onto the cable.
- Treating a joint and a termination as one line item. They have different interfaces, different cable-box constraints and different test evidence.
- Leaving screen and armour bonding parts to the contractor. Continuity of the metallic screen is a fault-current path, not a detail; the materials for it belong in the kit.
- Accepting a family type-test report as evidence for the ordered model. Ask for the report that names the model, the voltage class and the date.
Frequently Asked Questions About Cable Jointing
What is a joint kit used for?
It joins two lengths of power cable permanently — in a joint bay, a trench or a duct — restoring the conductor, the insulation, the screen and the armour. Kits are also used to replace a damaged section of cable after a fault.
What is the difference between a cable joint and a cable termination?
A joint connects cable to cable in the middle of a run. A termination connects the cable end to equipment such as a transformer, a switchgear panel or a metering cubicle, or to an overhead line. Both are supplied as kits sized to the cable.
How do I choose the right size of joint kit?
Start from the cable, not the voltage: conductor material and cross-sectional area, the number of cores, the insulation type and the diameter over the insulation. Manufacturers publish ordering tables that map each kit model to a cross-sectional area band, and those tables are the correct place to confirm the selection.
Which joint technology is best: heat-shrink, cold-shrink or pre-moulded?
All three work when they are installed correctly. Cold-shrink systems need no heat source, have fewer installation steps and keep constant radial pressure on the cable, which reduces the dependence on installer technique. Heat-shrink is widely available and familiar but depends on correct heating and surface preparation. The right answer usually follows the skill of the crew and whether hot work is permitted on site.
Can a joint kit be used for direct burial?
Only if the joint is specified for it. Direct burial, especially where the water table is high or the ground is contaminated, places sealing and moisture-barrier demands on the joint that an in-air or ducted joint does not face. State the burial condition in the RFQ and ask for a joint specified for that service.
What standards apply to a cable joint?
In the IEC system the cable and the accessory are covered by different documents: the cable part sets construction, dimensions and test requirements for extruded-insulation cables up to 30 kV, while accessory test requirements and accessory test methods sit in their own standards. Utility specifications usually add national or IEEE joint standards on top. Ask the supplier which document and edition the joint is type-tested to.
Why do cable joints fail?
Most failures trace back to the installation rather than to the materials: the wrong accessory selected, instructions that are hard to follow, too many steps, poor workmanship, or moisture and voids left inside the joint. Failures also occur where the stress-control parts at the screen cut-back are not fitted exactly as the manufacturer requires.
Sources and Further Reading
- IEC 60502-2 — power cables with extruded insulation and their accessories, rated 1 kV up to 30 kV; the cable-side standard and its exact title
- IEC 61442 — test methods for accessories for power cables rated 6 kV up to 30 kV, including the AC, impulse, partial-discharge and thermal short-circuit tests
- Egyptian Electricity Holding Company — specification for cable joints, XLPE insulated cables 12/20 (24) kV — joint type definitions, the applicable-standards table and the screen and armour bonding clauses
- Accessory manufacturer comparison of MV cable jointing technologies — heat-shrink, cold-shrink and pre-moulded systems described side by side, including stress control at the screen cut-back
- Cable accessory failure modes (specialist MV/HV accessory distributor) — the reliability factors listed in the section above
A joint kit is a small purchase against the cost of the cable run it protects, and it is the only part of that run assembled on site. Specify it against the cable, not against the voltage; insist on the type-test report for the exact model; and choose the technology your crews can install consistently. Those three decisions do more for network reliability than any comparison of kit prices.
Nahu Group (NAHU Electric Technology) manufactures cold-shrink cable accessories, including intermediate connections and terminations for 0.6/1 kV multicore cable and for higher-voltage three-core classes, alongside its current and voltage transformers, metering boxes and medium-voltage switching equipment. Browse the cable accessories range, read cold shrink vs heat shrink cable terminations or european-style cable branch boxes, or send the cable details for a kit recommendation.
Published September 29, 2026 · Nahu Group (NAHU Electric Technology)